Leave Your Message
Engineered for high-volume club store display, industrial dry food storage, and automated packaging systems. Bridging robust transport protection with high-impact shelf aesthetics.
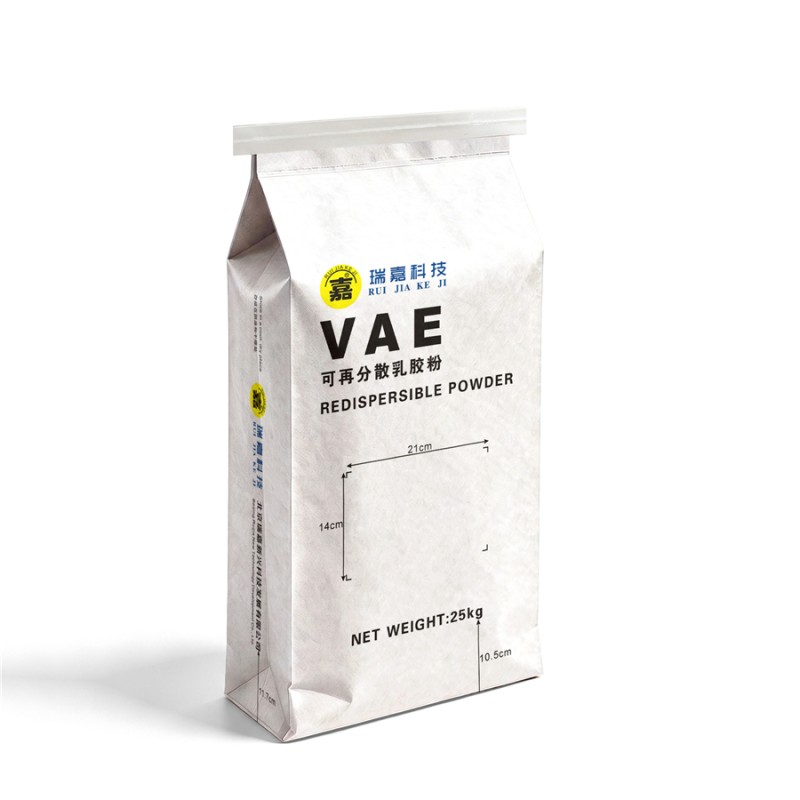
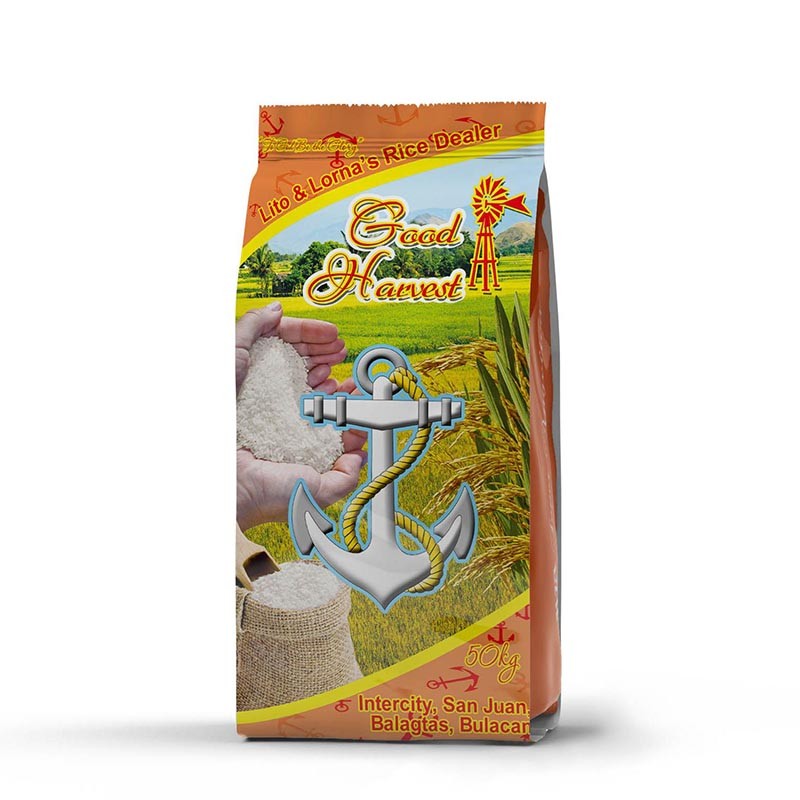
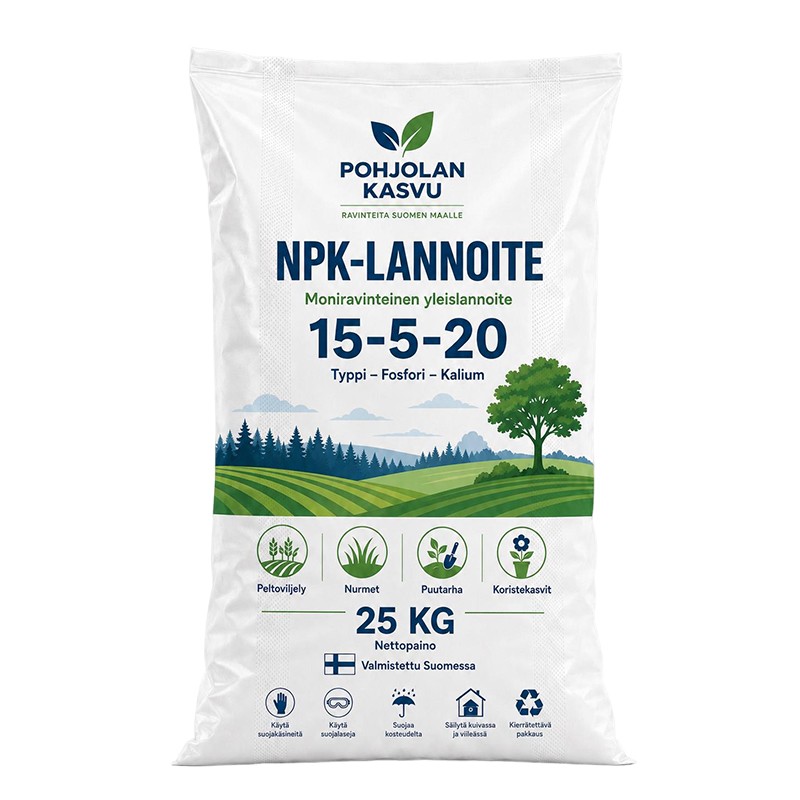
From industrial warehouses directly onto hypermarket pallet displays: Discover how multi-layer engineered film packaging is drastically lowering secondary corrugate costs, slashing logistics carbon footprints, and unlocking unprecedented shelf appeal for high-payload goods.
Global wholesale clubs and mass retailers (Costco, Sam's Club, Metro) have redefined product display metrics. Bulky 10kg to 25kg dry food products, pet nutrition, and home-improvement consumables are moving from secondary cardboard boxes directly to primary retail-ready film sacks. Custom printed high-gloss films eliminate unboxing labor while showcasing photographic brand graphics that drive higher impulse buy conversion.
By transitioning from rigid corrugated outers and generic multi-wall paper sacks to engineered co-extruded heavy-duty PE films, global packagers realize between 28% and 42% volume reduction in shipping cubes. Thin-gauge, ultra-tough mPE (metallocene polyethylene) formulations minimize tare weight, reduce dunnage waste, and maximize intermodal shipping container payloads across transatlantic and transpacific trade lanes.
Regulatory mandates across the European Union (PPWR) and North America prioritize mono-material polyolefin constructions that fit into standard PE recycling streams (Code 4). Our heavy-duty barrier film solutions engineer oxygen and moisture vapor barriers directly into mono-oriented PE/EVOH-ready structures, reconciling mandatory sustainability goals with extreme shelf-life security.
Modern retail-ready bulk packaging must survive a hostile logistics journey: from automated robotic palletizers and rough marine voyages to forklift transit and multi-tiered retail floor stacking. Achieving structural integrity without sacrificing printing clarity demands advanced multi-layer polymer extrusion.
Our blown film lines utilize up to 7-layer and 9-layer co-extrusion technology, orchestrating virgin mPE, high-density polyethylene (HDPE), tie layers, and EVOH barriers into a unified composite matrix. This architecture provides unmatched dart drop resistance, flex-crack survival at sub-zero cold chain temperatures, and pinhole resistance against abrasive angular bulk materials.
Empirical comparison between conventional multi-wall kraft paper bags versus custom co-extruded retail-ready bulk PE film.
Retail-ready bulk film packaging addresses specific biochemical, environmental, and physical challenges across heavy commercial industries.
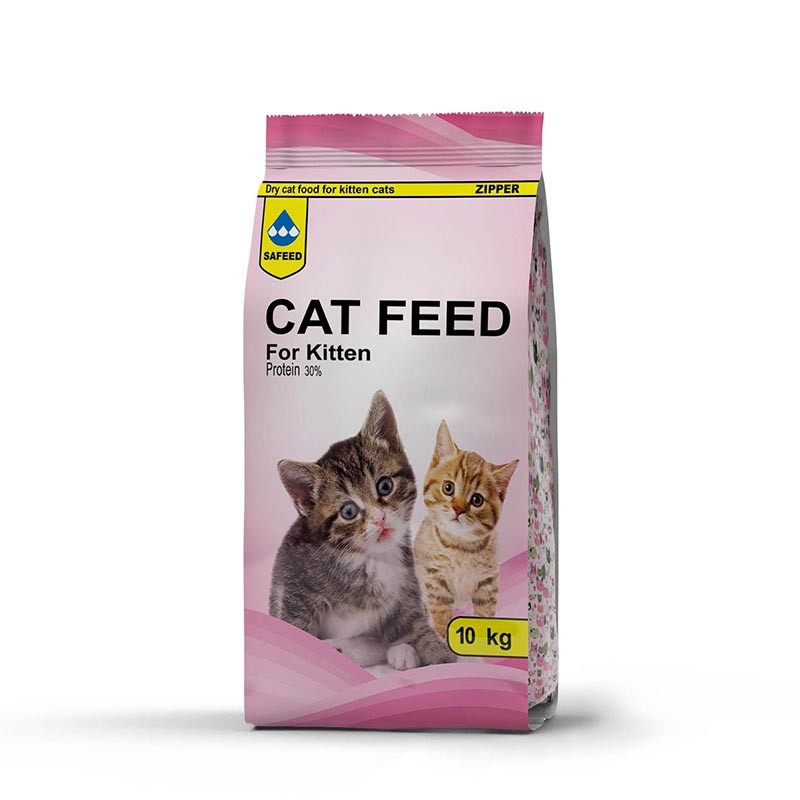
Pet food brands targeting wholesale clubs demand bags holding 12kg to 20kg that combine immaculate shelf presentation with total aroma preservation. High fat content in premium kibble often results in oil migration and rancidity when packed in unlined paper. Our multi-layer co-extruded barrier films prevent lipid oxidation, resist grease bleed-through, and incorporate hermetic slide-zippers or pocket-zippers for end-user convenience.
Anti-skid micro-embossing along the side gussets enables safe pallet stacking up to 3 pallets high without sliding during transit, safeguarding retail floor safety while displaying brilliant photorealistic packaging artwork.
Industrial baking flours, starches, maltodextrins, and bulk sugar supplied to bakeries and hypermarket cash-and-carry sectors require impenetrable humidity barriers. Atmospheric moisture creates clumping, bacterial growth, and mold inside traditional woven bags. Our laminated composite films feature hermetic hermetic seals and engineered labyrinth de-aeration channels that exhaust excess air without allowing airborne moisture or pests inside.
Certified food-grade contact layers complying with EU 10/2011 and FDA food contact regulations ensure absolute taste purity and zero contaminant migration across extended 24-month supply chains.
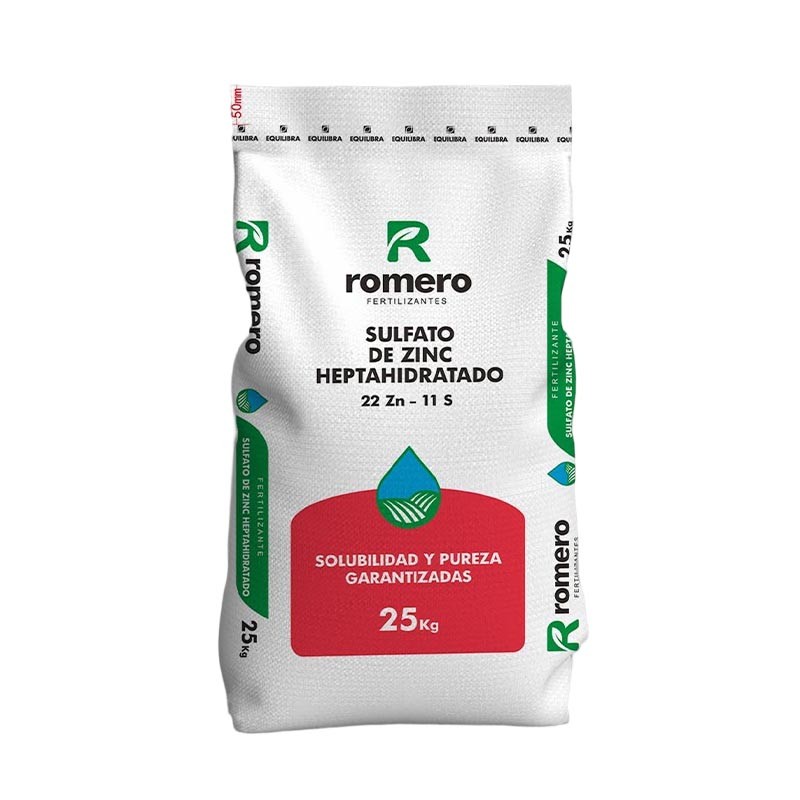
Lawn fertilizer blends, decorative garden soil, and specialty water-soluble nutrients sold in home improvement centers often face outside nursery storage exposed to torrential rain and intense solar UV radiation. Conventional paper-plastic combinations rot or fade within weeks.
We infuse heavy-duty PE films with advanced hindered amine light stabilizers (HALS) and anti-UV blockers guaranteeing up to 12 months of direct open-air solar resistance. Brilliant surface flexo printing remains vivid and non-chalking, protecting retail curb appeal even after weeks of outdoor pallet exposure.
High-tech polymers such as EVOH, PA66, and specialty compound masterbatches are inherently hygroscopic and chemically vulnerable. Even fractional atmospheric moisture absorption ruins injection molding processes downstream. In warehouse-club commercial hardware sectors, chemical powders require puncture-immune packaging that protects warehouse staff from hazardous dust leakages.
Our heavy-duty FFS films feature static-dissipative surfaces, high dart-drop values exceeding 1000g, and airtight ultrasonic bottom seals that eliminate product dusting and particulate contamination.
Combining factory-level production control with professional overseas trade execution for international clients across North America, Europe, Australia, and Southeast Asia.
Jinan Jiufen Import & Export Co., Ltd. operates as our dedicated international trade partner, working in close coordination with Fuyao Packaging.
While Fuyao focuses on world-class production, extrusion technology, and state-of-the-art manufacturing, Jiufen is responsible for all overseas business operations, including:
This integrated structure allows us to provide a complete supply chain solution, combining factory-level production control with professional export services, ensuring smooth and efficient transactions for global clients.
Our dual-engine model bridges production scale directly to foreign ports, eliminating broker layers and safeguarding specifications from polymer extrusion to container sealing.
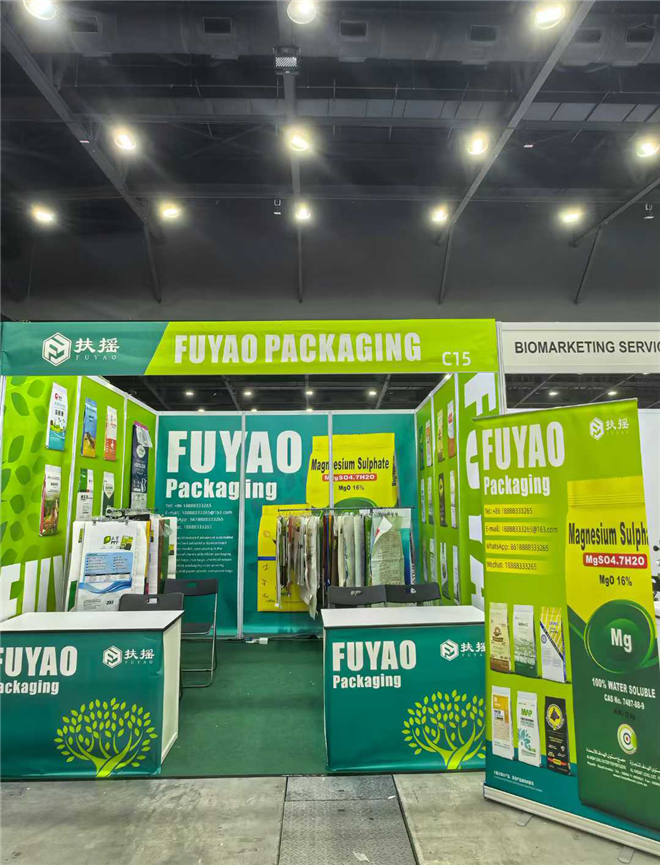
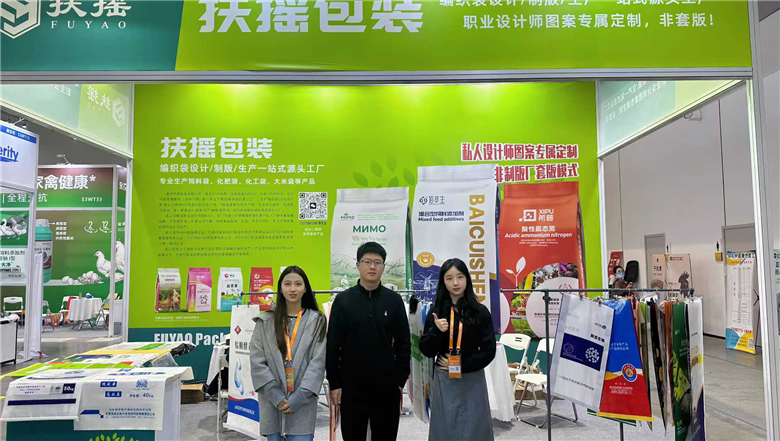
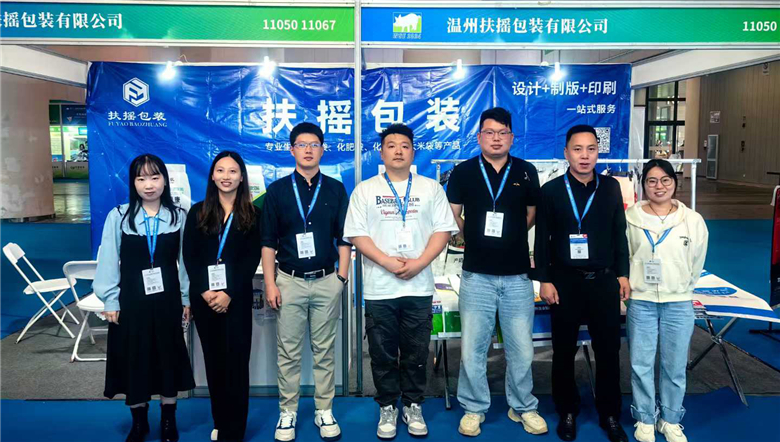
Connecting with packaging engineers, chemical distributors, and retail procurement leaders across major global expos and conventions.
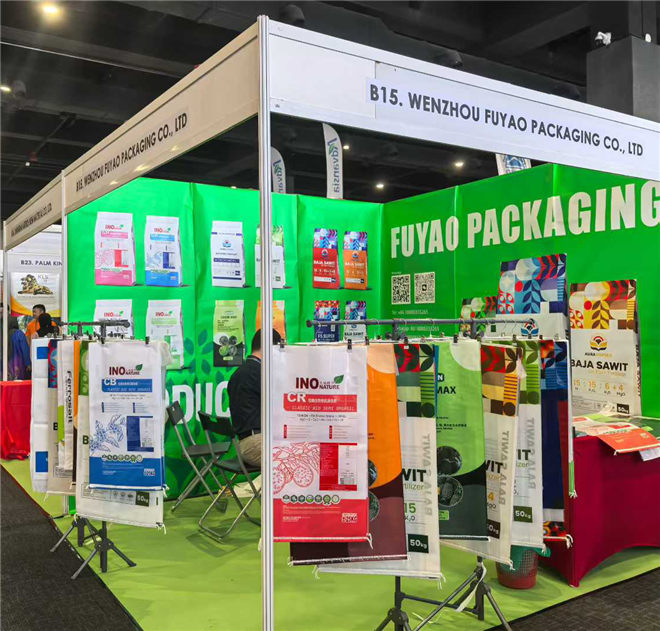
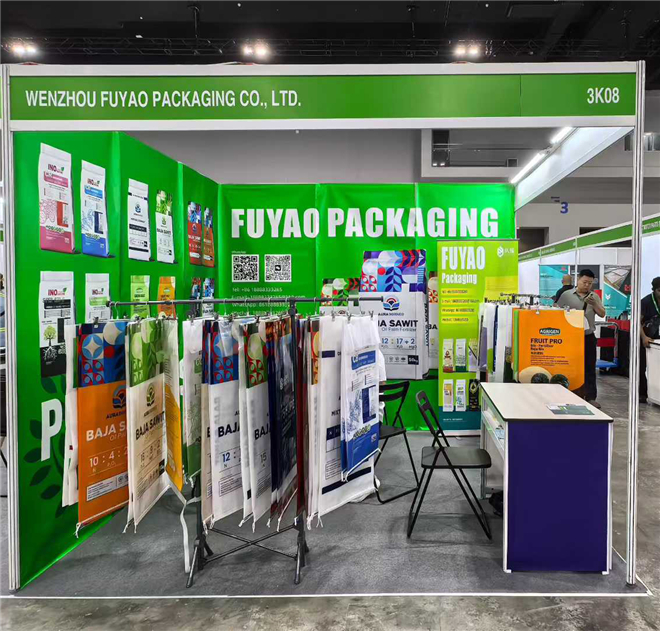
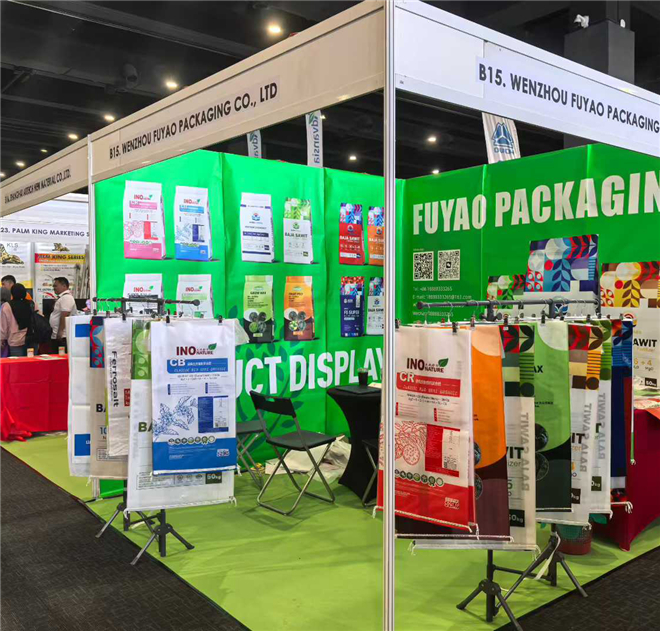
The name “Jiufen” originates from the concept of moderation in traditional philosophy, reflecting a business approach that values balance, humility, and continuous improvement. Rather than pursuing short-term gains, we focus on long-term cooperation and sustainable growth.

Over the years, we have built long-term partnerships with clients across various industries, providing customized packaging solutions tailored to specific applications.
By combining strong manufacturing capability with professional export services, we aim to deliver reliable products, competitive solutions, and consistent support to customers worldwide.

We are committed to deepening our presence in international markets and building a trusted global trade brand through high-quality products and professional service, achieving steady and sustainable growth across evolving industrial sectors.
As a technology-driven and environmentally responsible manufacturer, we integrate R&D, production, sales, and service into one unified system. We continuously invest in innovation to enhance product performance, reduce environmental impact, and pioneer recyclable bulk film alternatives.
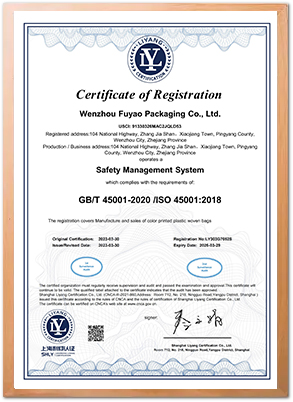
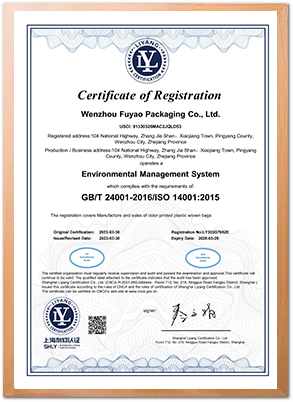
Our company has been recognized as an AAA Credit Enterprise and has obtained multiple authoritative international certifications:
These certifications demonstrate our strict quality control, continuous batch verification, and compliance with the most demanding global standards.
Engineered for mission-critical containment, high tensile strength, and high-resolution custom print branding across industrial, agricultural, and retail applications.