Leave Your Message
Engineered for extreme durability, moisture barrier protection, and high-definition branding.
How modern heavy-duty packaging bridges the gap between industrial logistics and retail merchandising.
In the global supply chain, the boundary between industrial bulk storage and commercial retail display is rapidly dissolving. Historically, heavy-duty bags were designed solely for utility—to transport raw chemicals, construction minerals, agricultural feeds, and food ingredients from point A to point B without tearing. Aesthetics were a distant afterthought. Today, however, global market dynamics demand retail-ready bulk packaging. Businesses seek heavy-duty bags that not only withstand the rigors of automated palletization and rough logistics but also feature high-impact, custom-printed graphics that speak directly to consumers and commercial buyers on warehouse club shelves.
This paradigm shift has transformed the manufacturing requirements of packaging materials. Manufacturers are no longer just producing simple plastic sacks; they are fabricating complex, multi-layered structures capable of preserving product purity while acting as primary marketing vehicles. Whether it is premium pet food, landscape soil, specialized chemical resins, or dry construction mixes, the packaging must perform flawlessly under physical stress and look immaculate under retail lighting.
Engineered to survive drop tests, high-stack pressure, and dynamic friction during long-distance maritime and overland shipping.
Utilizing advanced flexographic and rotogravure printing to deliver vibrant colors, fine text, and barcode readability directly on the heavy-duty substrate.
Integrated moisture, oxygen, and UV barriers that prevent degradation of sensitive chemical powders, agricultural feeds, and hygroscopic materials.
A deep dive into the structural layers and technologies that define high-strength packaging.
Modern heavy-duty bags are rarely made from a single material. To achieve the optimal balance of puncture resistance, tensile strength, and barrier properties, we employ multi-layer co-extrusion technology. By combining linear low-density polyethylene (LLDPE) for flexibility and impact absorption with high-density polyethylene (HDPE) for structural stiffness, we create a robust core. For specialized chemical applications, additional barrier layers such as EVOH (Ethylene Vinyl Alcohol) or polyamide (Nylon) are laminated to prevent gas migration and volatile organic compound (VOC) leakage.
The synergy of paper and plastic offers the best of both worlds. The outer kraft paper layer provides an excellent, high-friction, flat surface for premium custom printing and retail display, while the inner plastic liner (often high-strength PE) ensures absolute water resistance and containment. This configuration is widely adopted in the premium animal feed and dry chemical sectors, where brand presentation is as critical as moisture protection.
In automated warehousing environments, pallet stability is paramount. Heavy-duty bags are treated with specialized anti-skid varnishes or embossed with micro-textures. This increases the coefficient of friction between stacked bags, preventing shifting, sliding, and subsequent product loss during forklift transport and high-rack storage. This tech-driven approach minimizes warehouse accidents and optimizes vertical space utilization.
How custom printed heavy-duty bags solve critical challenges across diverse industries.
Chemical powders and granular resins are highly sensitive to ambient humidity. A minor moisture ingress can cause clumping, rendering the raw materials unusable for injection molding or chemical processing. Our custom chemical packaging bags feature hermetically sealed valve closures and moisture-resistant barrier laminates. The exterior is custom printed with precise hazard communication symbols (GHS compliant), batch tracking QR codes, and corporate branding, ensuring safety compliance and instant brand identification on the factory floor.
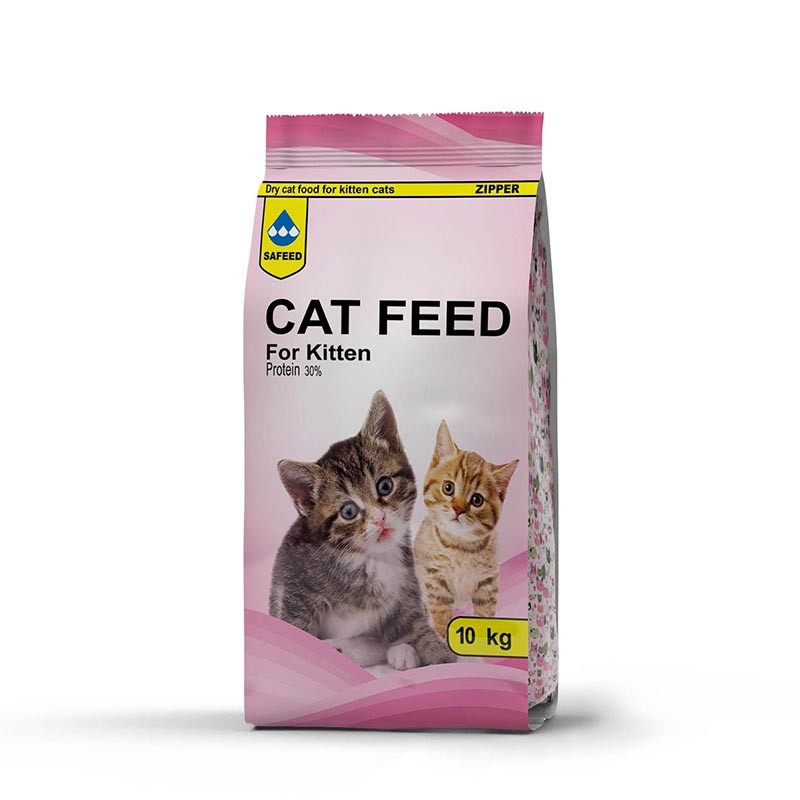
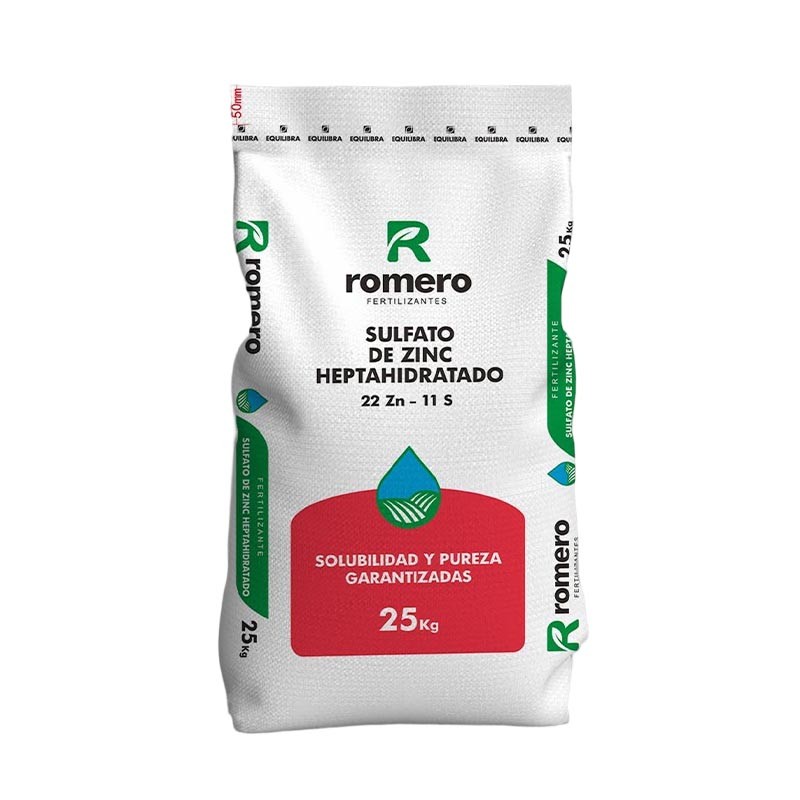
The agricultural sector has transitioned from plain woven sacks to highly branded, retail-ready bulk packaging. Premium horse feeds, organic fertilizers, and specialty seeds are sold directly to consumers in large farm supply stores. The packaging must withstand outdoor storage conditions (UV exposure and rain) while retaining its vibrant printed graphics to attract buyers. Our heavy-strength feed packaging bags incorporate UV inhibitors within the polymer matrix, preventing bag degradation and ink fading under direct sunlight.
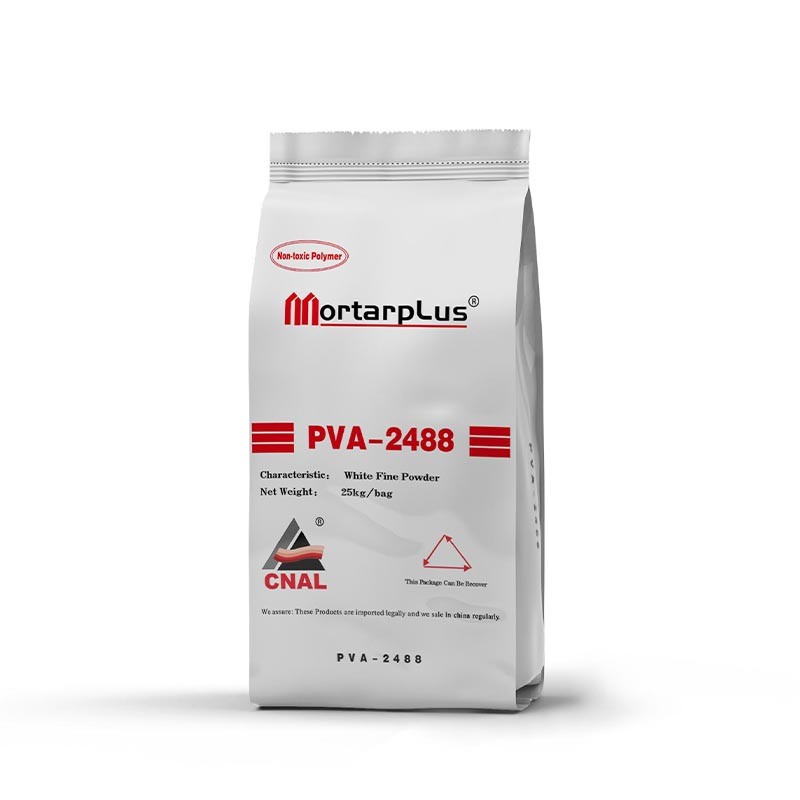
Fine powders like cement, grout, and silica sand require packaging that prevents dusting during handling while allowing air to escape during high-speed filling. By utilizing micro-perforation technology, our bags allow air to vent during the packaging process while keeping the fine powder securely contained. The tough outer layer resists the abrasive nature of minerals, ensuring the bags arrive at construction sites or retail home improvement centers intact and clean.
Embracing circular economy, advanced automation, and smart tracking systems.
The global push for sustainability is redefining the packaging industry. Traditional multi-layer bags containing different plastic types (e.g., PET laminated with PE) are difficult to recycle. The industry is rapidly shifting toward mono-material structures—such as packaging made entirely from polyethylene (PE) formulations that offer high barrier performance while remaining fully recyclable in standard recycling streams. Implementing PCR (Post-Consumer Recycled) resins into the core layers of heavy-duty bags is another major trend, allowing companies to reduce their carbon footprint without sacrificing mechanical properties.
IoT and smart logistics are making their way into bulk packaging. By integrating printed QR codes, RFID chips, or NFC tags directly onto custom-printed heavy-duty bags, manufacturers can achieve end-to-end supply chain visibility. Warehouse operators can scan entire pallets instantly, tracking batch numbers, manufacturing dates, and shipping destinations. This level of digitalization prevents counterfeiting, optimizes inventory management, and guarantees product authenticity for high-value chemical and agricultural products.
As industrial filling lines become more automated, packaging must adapt. Modern heavy-duty bags are designed with precise structural tolerances to ensure seamless integration with automatic bag hangers, ultrasonic sealing stations, and robotic palletizers. The bags must open reliably, fill without tearing, and seal instantly at high temperatures. Engineering bags with optimized stiffness and flat surfaces ensures that automated machinery operates at peak efficiency, minimizing downtime and labor costs.
The name “Jiufen” originates from the concept of moderation in traditional philosophy, reflecting a business approach that values balance, humility, and continuous improvement. Rather than pursuing short-term gains, we focus on long-term cooperation and sustainable growth.

Over the years, we have built long-term partnerships with clients across various industries, providing customized packaging solutions tailored to specific applications. By combining strong manufacturing capability with professional export services, we aim to deliver reliable products, competitive solutions, and consistent support to customers worldwide.

We are committed to deepening our presence in international markets and building a trusted global trade brand through high-quality products and professional service, achieving steady and sustainable growth.
Connecting with global industry leaders and showcasing our latest heavy-duty packaging innovations.
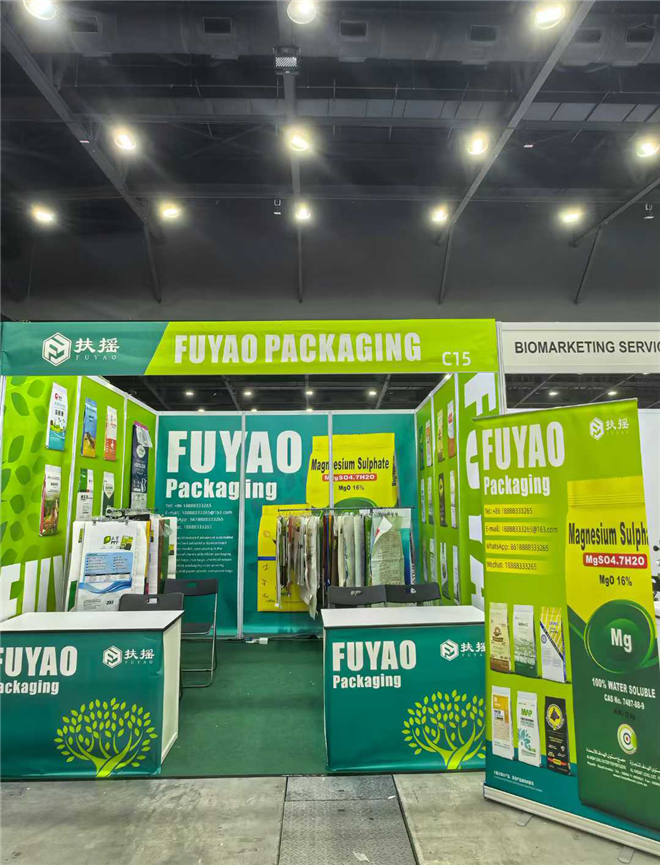
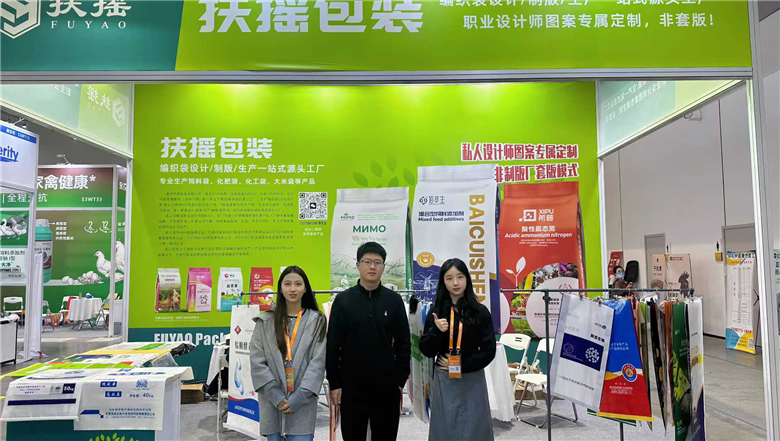
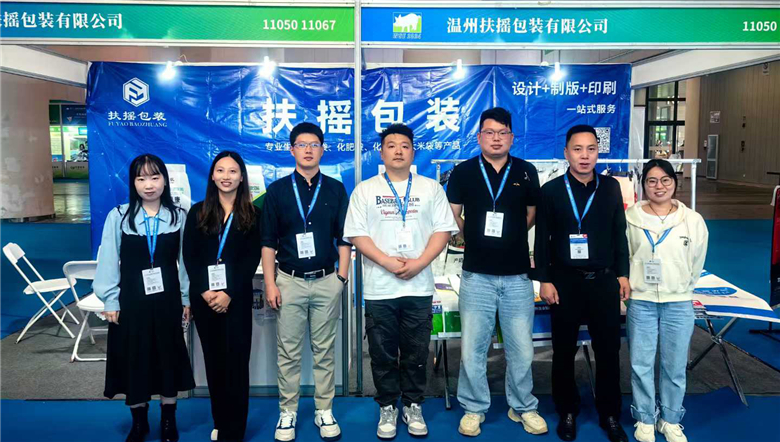
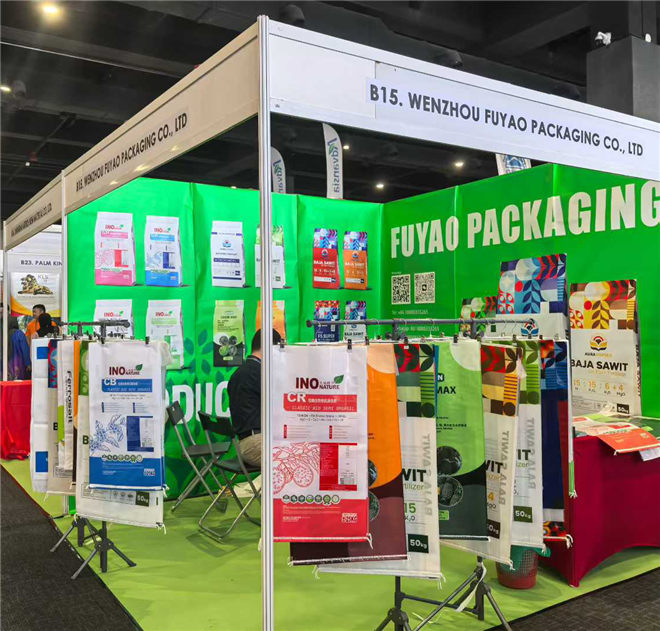
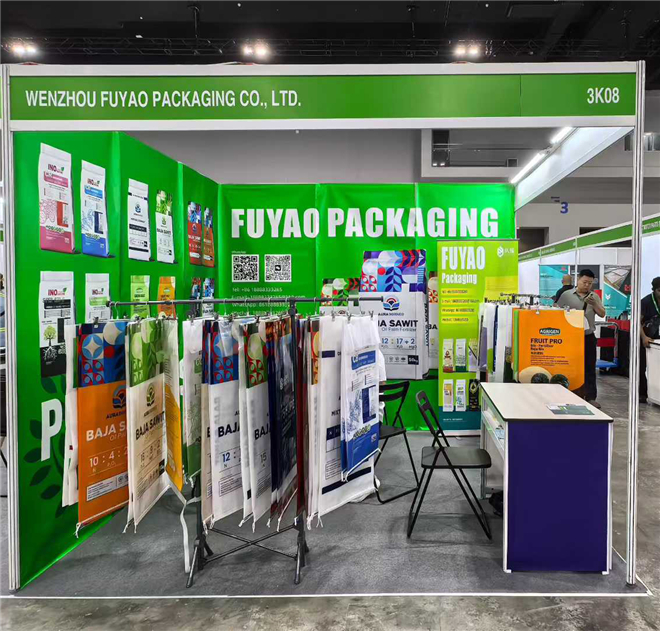
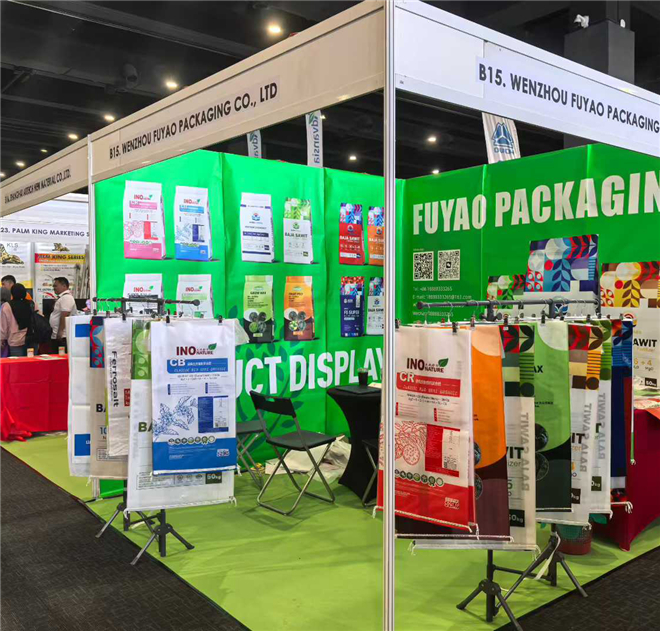
As a technology-driven and environmentally responsible manufacturer, we integrate R&D, production, sales, and service into one system. We continuously invest in innovation to enhance product performance and reduce environmental impact.
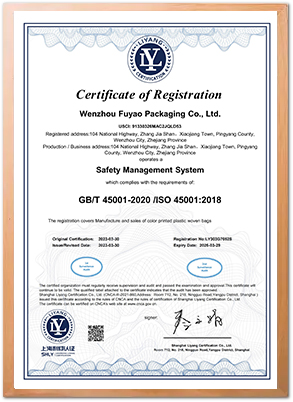
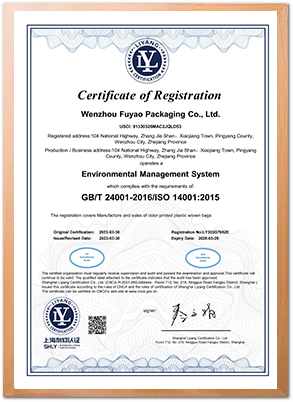
Our company has been recognized as an AAA Credit Enterprise and has obtained multiple international certifications:
These certifications demonstrate our strict quality control and compliance with global standards.
Explore our full range of heavy-duty bags designed for custom printed retail-ready bulk packaging.