Leave Your Message
Explore our top-tier packaging products designed to meet the rigorous logistics and preservation demands of American industrial, chemical, and agricultural sectors.
The United States is currently experiencing a monumental shift in its packaging sector. Traditional rigid containers, such as metal cans, glass jars, and heavy plastic tubs, are rapidly being replaced by high-performance seal packaging pouches. From the agricultural heartlands of the Midwest to the chemical corridors of the Gulf Coast, and the sprawling organic food markets of the West Coast, the demand for flexible packaging has reached unprecedented heights.
This transformation is driven by several key factors: the need to reduce carbon footprints, minimize transportation costs, and extend product shelf lives without relying on artificial preservatives. Modern manufacturing facilities across the US are upgrading their packaging lines to integrate Form-Fill-Seal (FFS) systems, which require premium, high-integrity pouches that can withstand extreme shipping conditions and automated handling.
"By transitioning from rigid containers to flexible seal packaging pouches, US manufacturers can achieve up to a 70% reduction in transportation-related carbon emissions and a 40% reduction in packaging material weight."
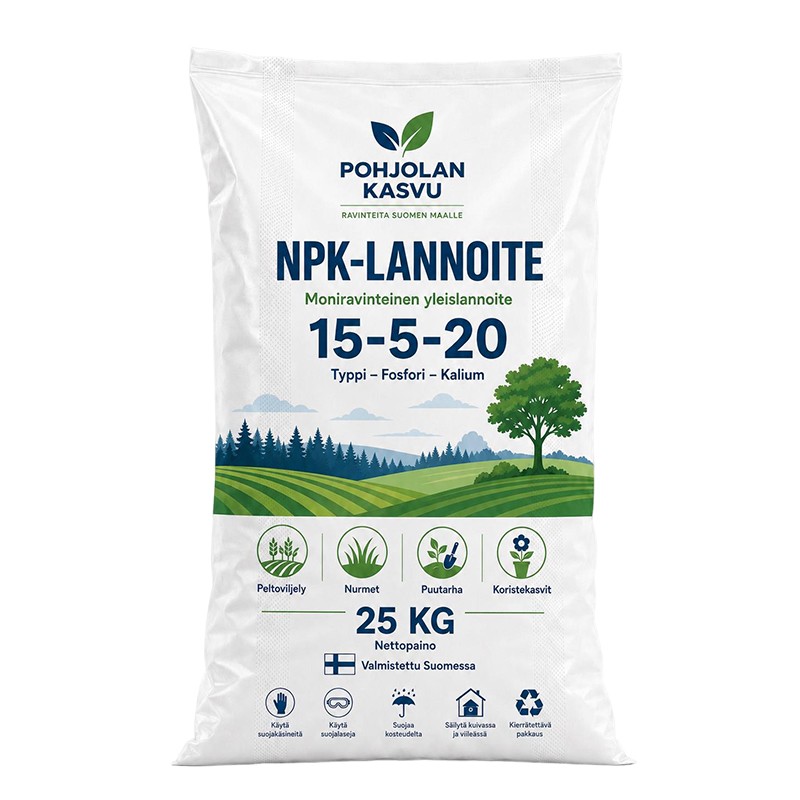
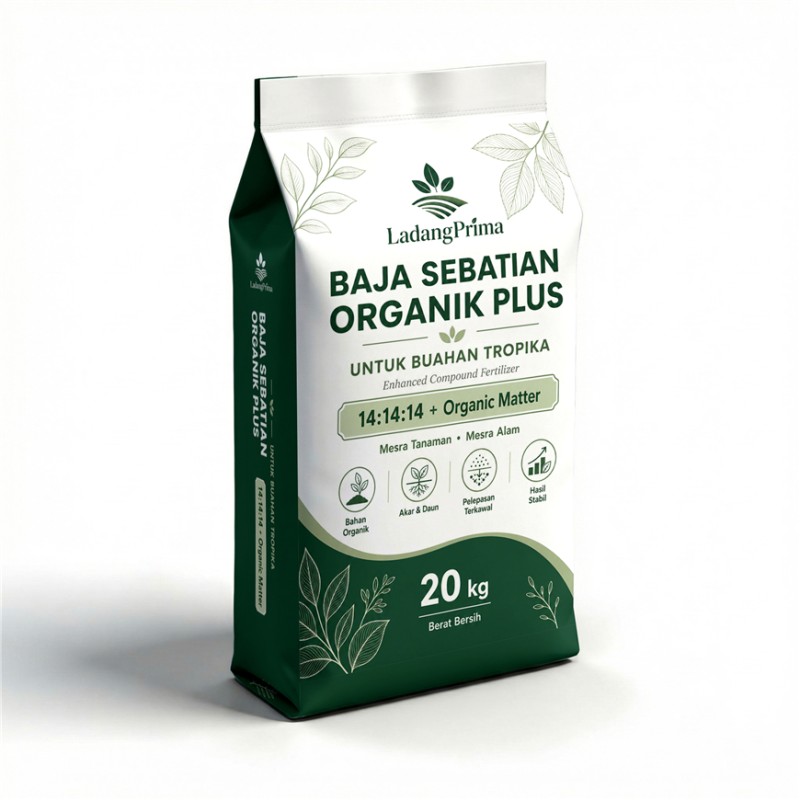
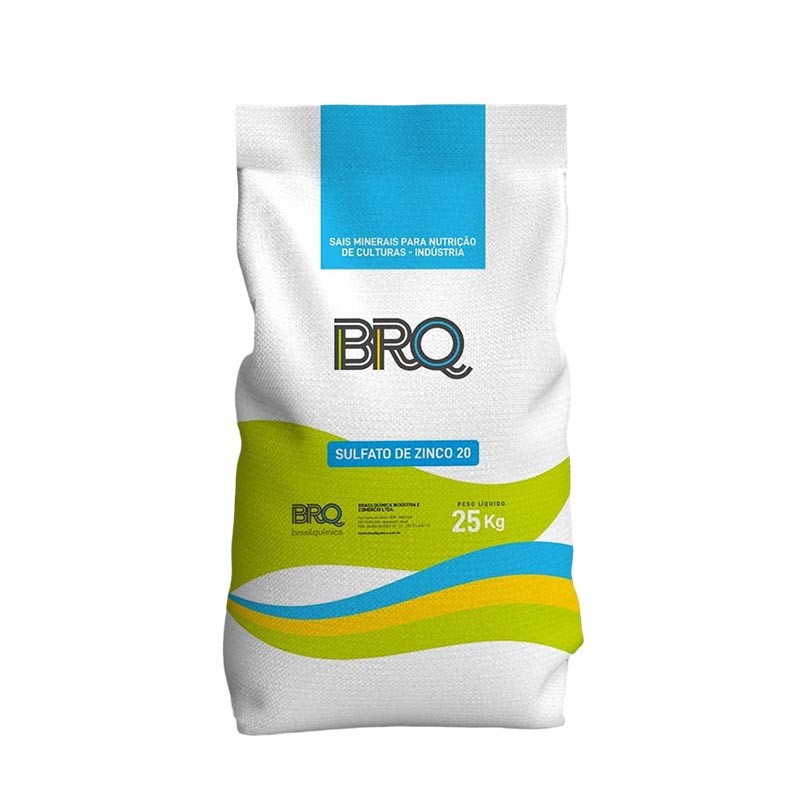
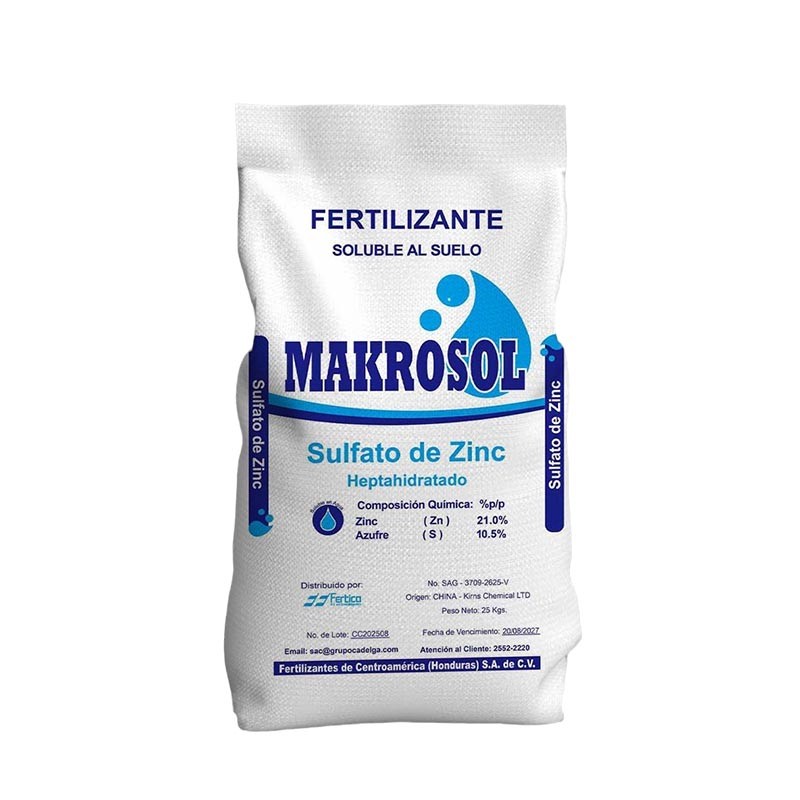
1. Midwestern Agricultural Hubs: Large-scale farms and agricultural cooperatives in states like Iowa, Illinois, and Nebraska require heavy-duty, moisture-resistant bags for animal feed, fertilizers, and seed grains. Laminated PP woven bags and PE FFS rolls are critical to preventing spoilage due to humidity and rain during open-air storage.
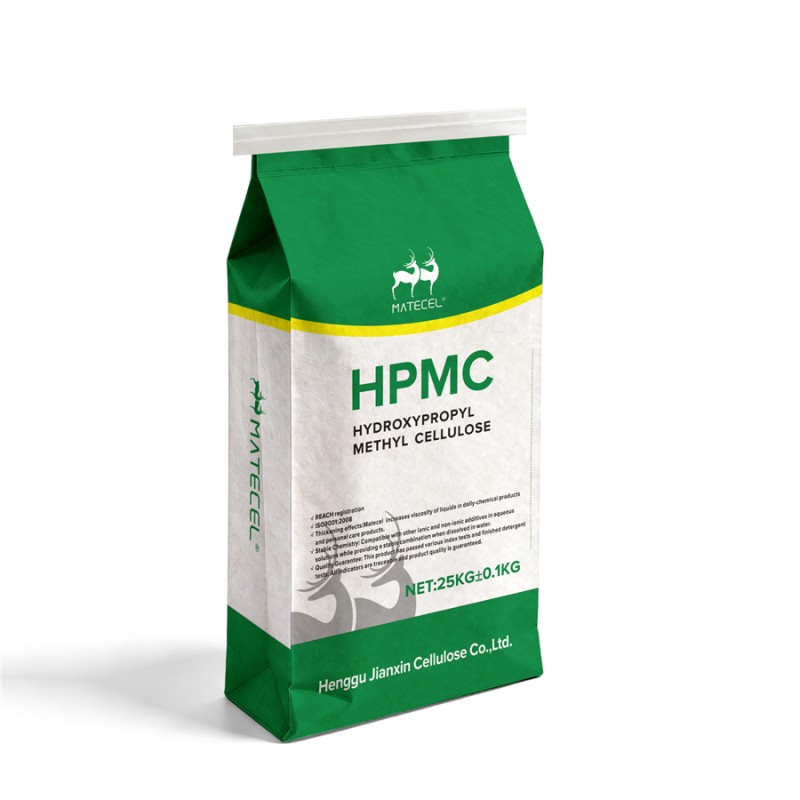
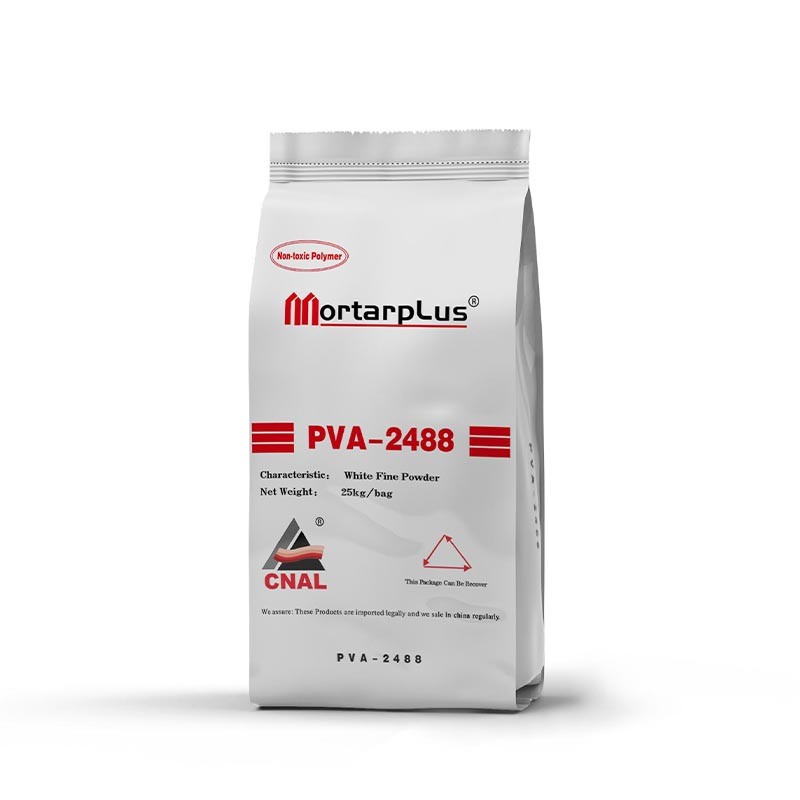
2. Gulf Coast Chemical & Petrochemical Plants: Texas and Louisiana house some of the world's largest chemical production plants. Packaging raw resins, hazardous powders, and industrial minerals demands specialized paper-plastic composite bags with high-barrier inner liners that prevent environmental contamination and product leakage.
3. Food & Beverage Processing: From artisanal coffee roasters in Seattle to organic grain packagers in California, food-grade laminated pouches certified under strict safety guidelines (like FDA and QS) are essential. These pouches preserve freshness, block UV light, and feature recloseable zippers for consumer convenience.
As sustainability and automation redefine manufacturing, seal packaging pouch technology is evolving to meet new regulatory and market standards.
Historically, multi-layer laminated pouches were difficult to recycle due to the challenge of separating different plastics (like PET, PE, and Aluminum foil). Today, the US market is demanding 100% recyclable mono-material structures (such as all-PE pouches) that can be easily processed in existing recycling streams. Brands aiming for ESG compliance are actively sourcing these materials to appeal to eco-conscious American consumers.
High-speed manufacturing lines in the United States rely heavily on automation. FFS (Form-Fill-Seal) machines require packaging films with consistent coefficient of friction (COF), precise thickness tolerances, and excellent heat-sealing properties. Furthermore, the integration of QR codes and RFID tags directly onto the pouch surface allows for real-time supply chain tracking, helping companies combat counterfeiting and streamline inventory management.
Protecting sensitive materials from oxygen, moisture, and light is paramount. Innovations in EVOH (Ethylene Vinyl Alcohol) co-extruded films and metallized barriers allow seal packaging pouches to achieve shelf-life extensions comparable to traditional metal and glass packaging, but at a fraction of the weight and cost.
Understanding cost structures is critical for procurement managers. Below is an indicative pricelist based on material composition, volume, and application requirements for the US market.
| Pouch Type / Material | Key Industrial Application | Typical Size / Capacity | Est. Price Range (USD/Unit)* | Minimum Order Qty (MOQ) |
|---|---|---|---|---|
| Paper-Plastic Composite | Chemical powders, flour, starches | 25 kg / 50 lbs | $0.45 - $0.85 | 10,000 pcs |
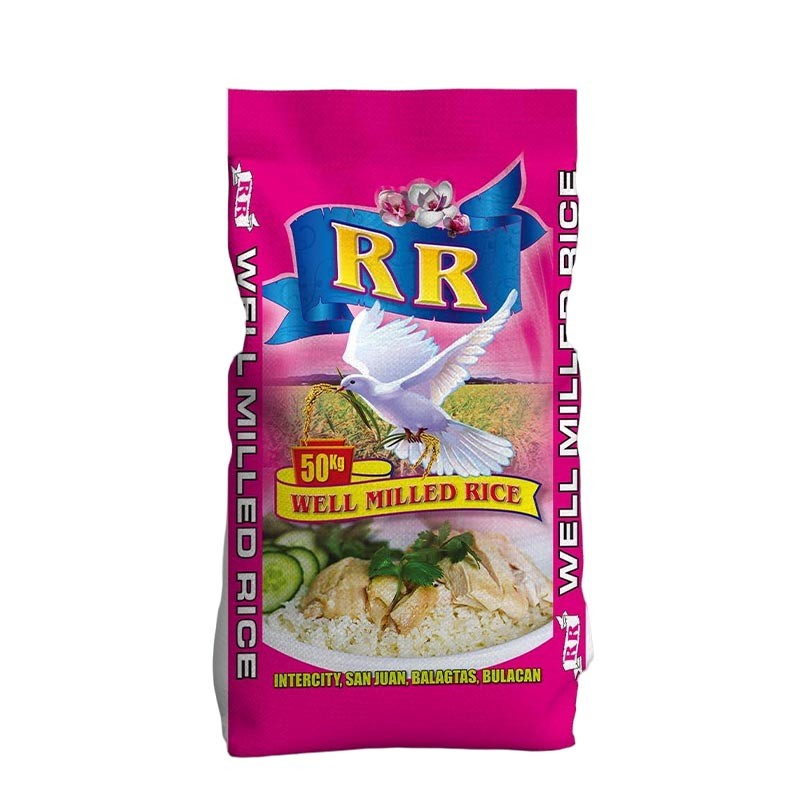
| BOPP Laminated PP Woven | Animal feed, fertilizers, grains | 20 kg - 50 kg | $0.35 - $0.70 | 10,000 pcs |
| Heavy-Duty PE FFS Film | Automated soil, salt, urea packing | Continuous roll (per ton) | $1,800 - $2,500 / ton | 5 tons |
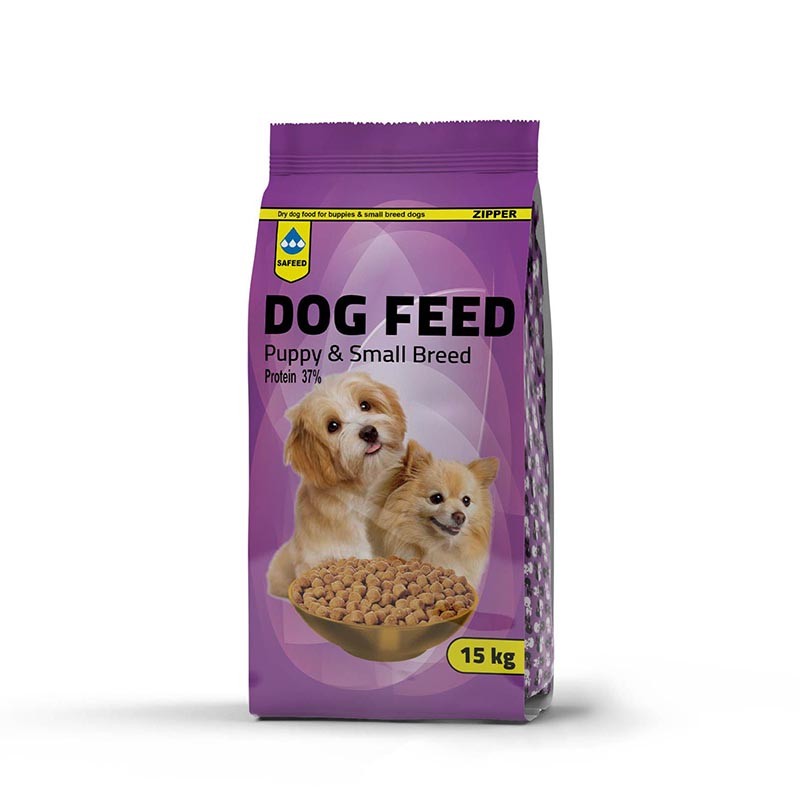
| High-Barrier Stand-Up Pouch | Pet food, food ingredients, resins | 1 lb - 5 lbs | $0.12 - $0.35 | 20,000 pcs |
| Aluminum Foil Multi-Layer | Sensitive chemicals, pharmaceuticals | Custom dimensions | $0.50 - $1.20 | 15,000 pcs |
*Note: Prices are estimates and vary based on custom printing requirements (gravure vs. flexo), barrier layers (EVOH, Alu), thickness, and freight options. Contact our sales department for a formal, customized quote.
Jinan Jiufen Import & Export Co., Ltd. operates as our dedicated international trade partner, working in close coordination with Fuyao Packaging.
While Fuyao focuses on production and manufacturing, Jiufen is responsible for all overseas business operations, including:
This integrated structure allows us to provide a complete supply chain solution, combining factory-level production control with professional export services, ensuring smooth and efficient transactions for global clients.
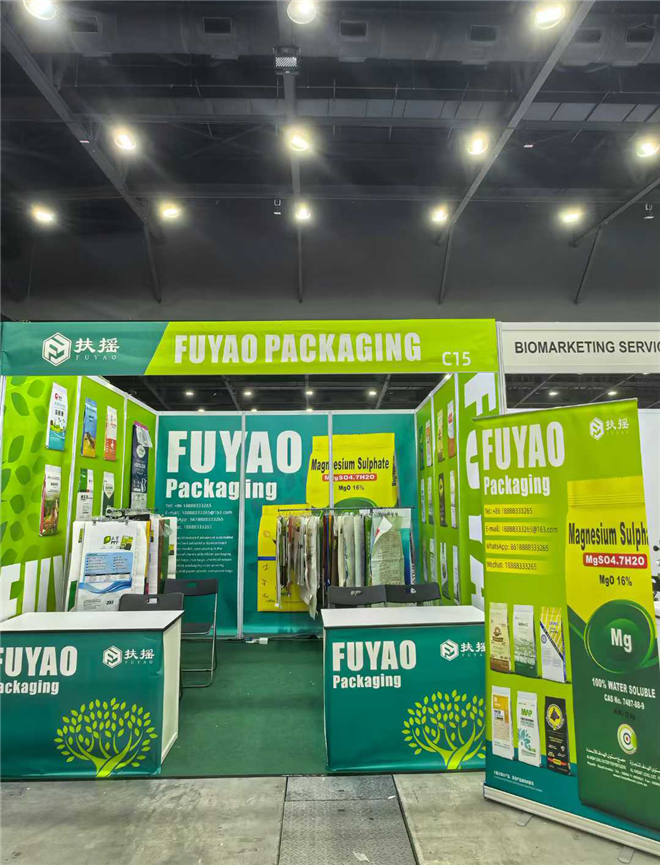
We actively participate in international packaging and industrial trade fairs to showcase our latest innovations and connect with partners globally.
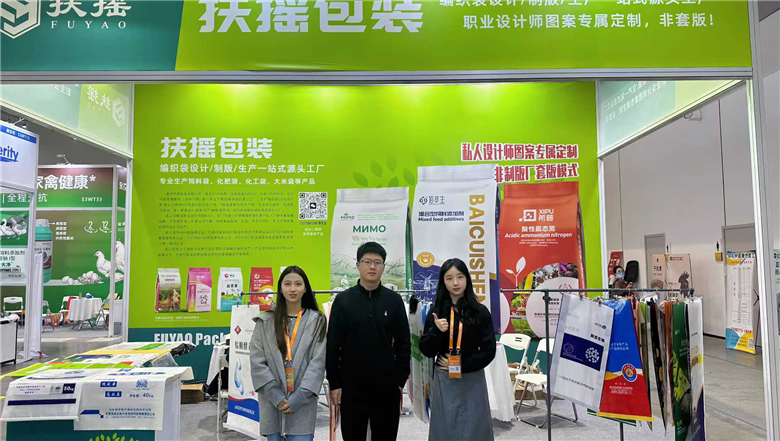
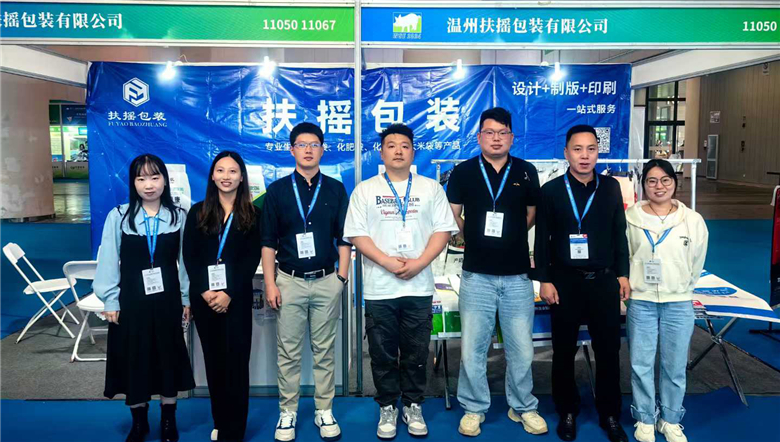
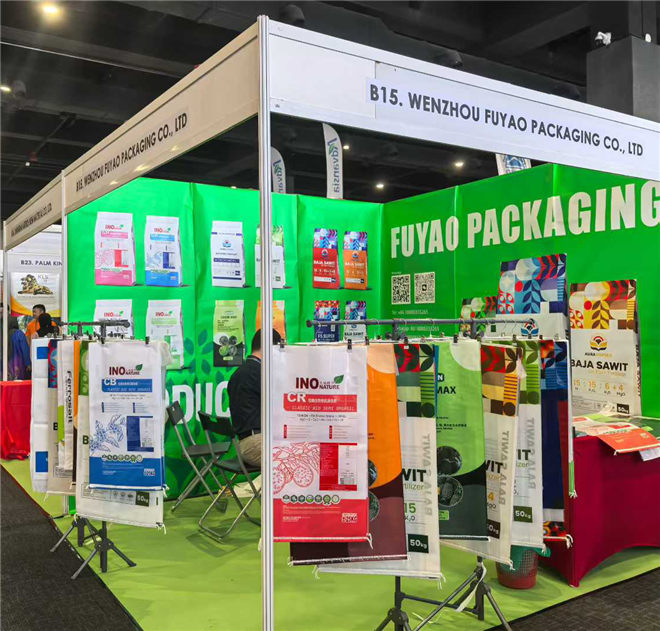
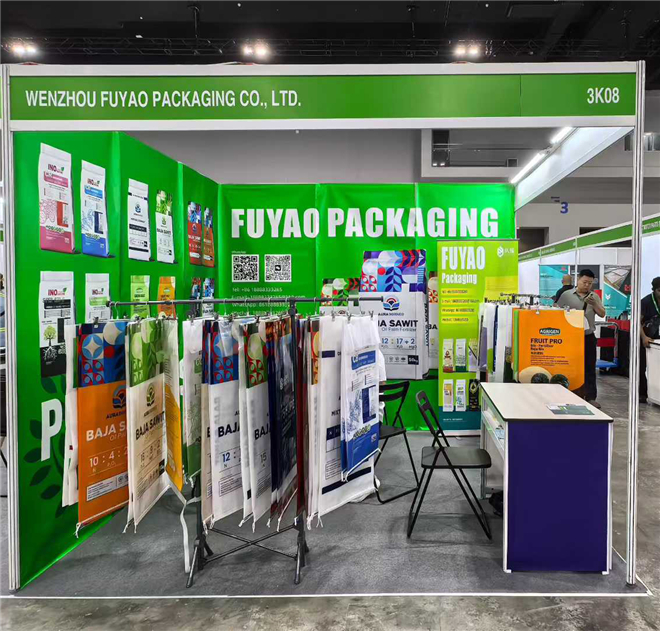
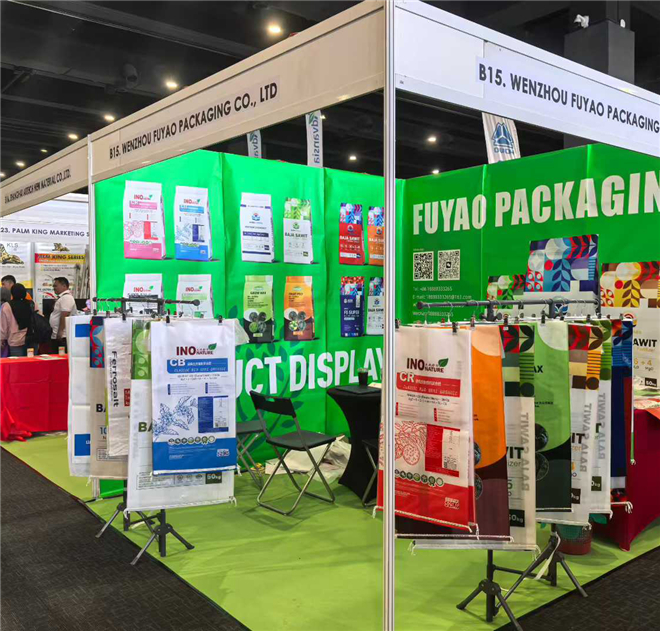
Guided by balance, long-term collaboration, and uncompromising quality in every pouch we produce.
The name "Jiufen" originates from the concept of moderation in traditional philosophy, reflecting a business approach that values balance, humility, and continuous improvement. Rather than pursuing short-term gains, we focus on long-term cooperation and sustainable growth.

Over the years, we have built long-term partnerships with clients across various industries, providing customized packaging solutions tailored to specific applications. By combining strong manufacturing capability with professional export services, we aim to deliver reliable products, competitive solutions, and consistent support to customers worldwide.

We are committed to deepening our presence in international markets and building a trusted global trade brand through high-quality products and professional service, achieving steady and sustainable growth.
As a technology-driven and environmentally responsible manufacturer, we integrate R&D, production, sales, and service into one system. We continuously invest in innovation to enhance product performance and reduce environmental impact.
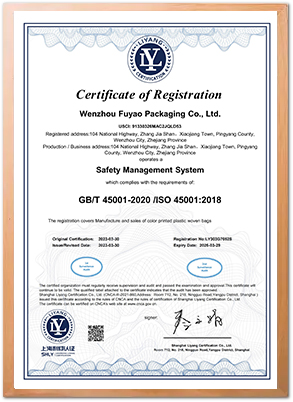
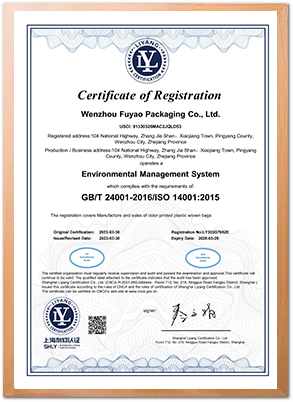
Our company has been recognized as an AAA Credit Enterprise and has obtained multiple international certifications:
These certifications demonstrate our strict quality control and compliance with global standards, ensuring that clients in the United States receive only the highest-grade packaging materials.
Browse our full range of heavy-duty composite bags, FFS films, and laminated packaging solutions designed for automated and manual sealing lines.